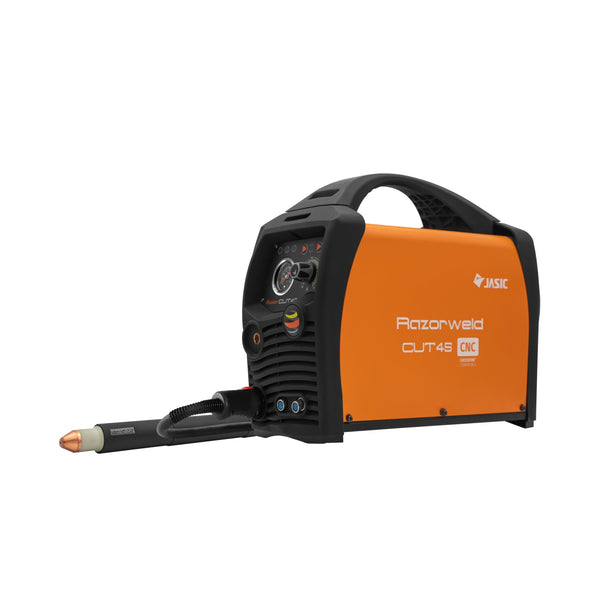
Razorweld Razorcut 45
Budget / light duty
$1,289
The most affordable way to cut steel up to 1/2" cleanly, for hobby and light shop work on any CrossFire.
- Clean cut
- 1/2"
- Duty cycle
- 30% @ 45 A
- Works with
- All CrossFire tables


Your CNC table moves the torch, but the plasma cutter decides how thick you can cut, how clean the edges are, and how long you can run between breaks. We sell four CNC-ready cutters from Razorweld and Hypertherm, each with a 25' torch, matched to the CrossFire tables they work with.
Pick the thickest steel you cut, the largest sheet you load, and how you'll use it. The finder only suggests cutters each CrossFire accepts.
Thickest mild steel you'll cut
Largest sheet you'll load
How you'll use it
Recommended setup
Every cutter below ships with a 25' torch and works with the CrossFire tables listed. Bundle one with a table order, or buy it on its own.
Budget / light duty
$1,289
The most affordable way to cut steel up to 1/2" cleanly, for hobby and light shop work on any CrossFire.
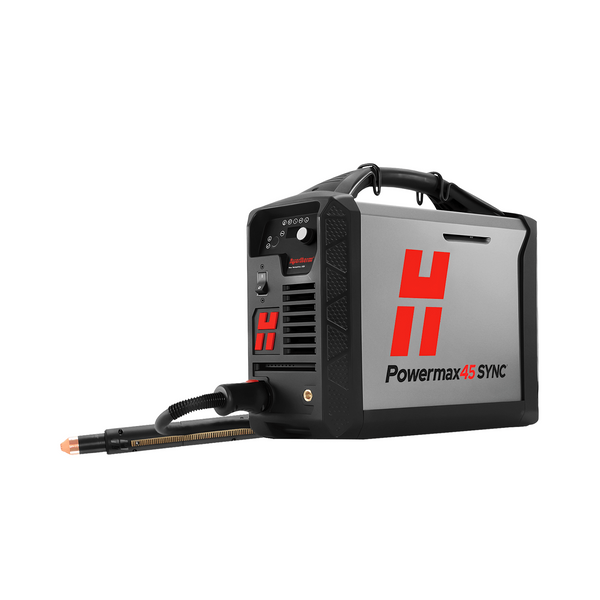
Pro standard
$3,300
Cleaner edges, a higher duty cycle, and lower air demand than the Razorcut. The best all-round choice for any CrossFire.
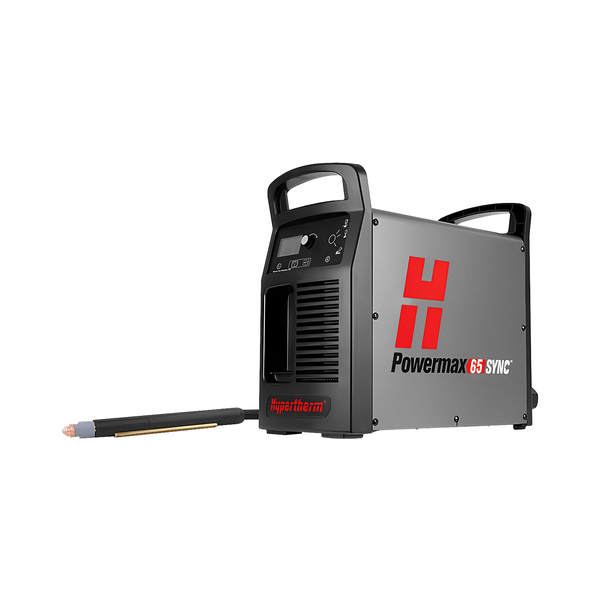
Heavy plate
$4,375
Clean cuts to 3/4" and faster cutting on thick plate, for the CrossFire PRO MAX and XR.
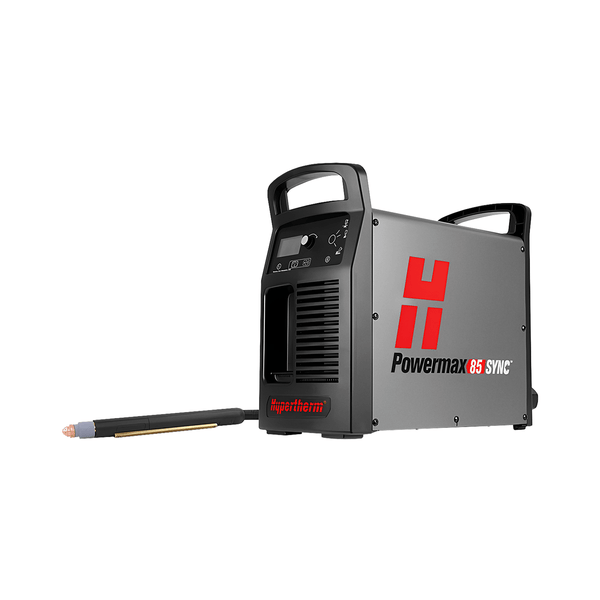
Maximum capacity
$5,650
Clean cuts to 1" and the highest duty cycle we offer, for production work on the CrossFire PRO MAX and XR.
| Model | Price | Output | Duty cycle | Air needed | Clean cut | Severance | Pierce | Works with |
|---|---|---|---|---|---|---|---|---|
| Razorweld Razorcut 45 | $1,289 | 20–45 A | 30% @ 45 A | 6.7 scfm @ 75 psi | 1/2" 12.7 mm | 5/8" 15.9 mm | 3/8" 9.5 mm | All CrossFire tables |
| Hypertherm Powermax45 SYNC | $3,300 | 20–45 A | 50% @ 45 A, 100% @ 32 A | 4 scfm @ 90 psi | 5/8" 15.9 mm | 1-1/8" 28.6 mm | 1/2" 12.7 mm | All CrossFire tables |
| Hypertherm Powermax65 SYNC | $4,375 | 20–65 A | 50% @ 65 A, 100% @ 46 A | 7.5 scfm @ 85 psi | 3/4" 19.1 mm | 1-1/4" 31.8 mm | 5/8" 15.9 mm | CrossFire PRO MAX and CrossFire XR |
| Hypertherm Powermax85 SYNC | $5,650 | 25–85 A | 50% @ 85 A, 100% @ 66 A | 7.5 scfm @ 85 psi | 1" 25.4 mm | 1-1/2" 38.1 mm | 3/4" 19.1 mm | CrossFire PRO MAX and CrossFire XR |
Clean cut is a production-quality cut at a good speed. Severance is the most the cutter can part, slowly and with rough edges. Pierce is the thickest plate it can start a hole in; thicker parts need an edge start. Duty cycle is how much of a 10-minute period the cutter can run at that output before it needs to cool.
The CrossFire, CrossFire XL and CrossFire PRO accept cutters up to 45A. The CrossFire PRO MAX and CrossFire XR accept every cutter on this page.
Razorcut 45
Pierce 3/8" · Clean cut 1/2" · Sever 5/8"
Powermax45 SYNC
Pierce 1/2" · Clean cut 5/8" · Sever 1-1/8"
Powermax65 SYNC
Pierce 5/8" · Clean cut 3/4" · Sever 1-1/4"
Powermax85 SYNC
Pierce 3/4" · Clean cut 1" · Sever 1-1/2"
Powermax45 SYNC
Pierce 1/2" · Clean cut 1/2"
Powermax65 SYNC
Pierce 1/2" · Clean cut 3/4"
Powermax85 SYNC
Pierce 5/8" · Clean cut 7/8"
Hypertherm doesn't rate severance for stainless steel or aluminum, so these tabs show pierce and clean cut only.
Powermax45 SYNC
Pierce 3/8" · Clean cut 5/8"
Powermax65 SYNC
Pierce 1/2" · Clean cut 3/4"
Powermax85 SYNC
Pierce 5/8" · Clean cut 1"
Hypertherm doesn't rate severance for stainless steel or aluminum, so these tabs show pierce and clean cut only.
Clean cut is a production-quality cut at a good speed. Severance is the most the cutter can part, slowly and with rough edges. Pierce is the thickest plate it can start a hole in; thicker parts need an edge start.
Six things decide whether a plasma cutter is right for CNC work. Get these right and you'll get clean parts without fighting your machine. Still choosing a table, too? Our CNC Plasma Table Buying Guide covers cost, size, and setup.
Pick the cutter whose clean-cut rating covers the thickest steel you cut every week, not once a year. Buying for severance means slow, rough cuts on your everyday work.
Duty cycle is the share of a 10-minute period a cutter can run at a given output. A 50% duty cycle at 45A means 5 minutes of cutting in every 10 at full power. For long nested jobs, choose a Hypertherm: each runs at 100% duty cycle at a lower output.
Plasma cutters need clean, dry air at a steady flow. Size your compressor to deliver the listed flow continuously, for example 4 scfm at 90 psi for the Powermax45 SYNC, and add a filter or dryer to protect your consumables.
A straight machine torch mounts in the CrossFire torch holder. The torch lead must be at least 16' on the CrossFire PRO and 25' on the CrossFire XR. Every cutter we sell includes a 25' machine torch.
The CrossFire fires the torch and, with torch height control, reads arc voltage from the cutter. The Razorcut 45 we sell is plug-and-play, and Hypertherm SYNC models connect through their CPC port. Cutters bought elsewhere may need to be wired by hand.
Electrodes and nozzles wear with every pierce. Hypertherm SYNC cutters combine them into a single cartridge, which makes changes faster. Keep a spare set on hand before a big job.
The CrossFire works with many plasma cutters besides the ones we sell. Check these requirements first, then find your model in the compatibility list below.
Your plasma cutter must use a blow-back start to create its pilot arc. High-frequency (HF) start cutters must never be used on a CrossFire: the HF arc can permanently damage the machine's electronics.
Most modern plasma cutters use blow-back start. If you're unsure about your model, ask its manufacturer how it starts the arc.
Some plasma cutters can run on 110V, but we only recommend 220V cutters for CrossFire tables. 110V cutters require standoff distances that are too short for CNC cutting.
The torch lead must be at least 16' long for the CrossFire PRO and 25' long for the CrossFire XR. If your lead is shorter, ask your plasma cutter's manufacturer whether they offer a torch with a longer lead.
Razorweld plasma cutters bought from other sellers are compatible with CrossFire CNC machines. However, you will likely have to wire them for torch firing and THC voltage by hand, since they are usually not plug-and-play despite having similar ports.
Splicing into the torch trigger wires may or may not violate your plasma cutter's warranty. It is your responsibility to check with your plasma cutter manufacturer regarding the terms of the warranty and whether or not executing the splicing procedure violates those terms. Langmuir Systems will not be held responsible for warranty violations.
Completing the procedure requires opening up the cabinet of your plasma cutter power supply, which will expose you to high voltage and high amperage electrical components. It is your responsibility to make sure that all work is done safely and with the power disconnected. If you have any doubts regarding your ability to safely perform this work, we strongly urge you to solicit the services of a professional electrician. Langmuir Systems will not be held responsible for any injury or death resulting from the incorrect or unsafe execution of this procedure.
After the wire splices are made, it is critical to never leave the torch firing cable connected to the CrossFire electronic enclosure when the torch is not installed in the torch mount and ready to cut. If the torch is required for hand cutting duty, it is imperative to first disconnect the torch firing cable before removing the torch. Failure to do so creates the opportunity for the CrossFire electronic system to turn the torch on when the torch is physically in an unsafe location, such as in the presence of volatile or explosive substances. Failure to disconnect the torch firing cable from the electronic enclosure when the torch is not installed can cause serious injury or death. Langmuir Systems will not be held responsible for any injury or death resulting from the lack of adherence to this critical safety requirement.
Interference from the power supplies of these cutters has been known to cause issues with CrossFire electronics:
Owners of these models who want to use them with a CrossFire must take further steps to ensure proper grounding and resistance to EMI. Use of these cutters is not supported by Langmuir Systems and is at your own risk.
Plasma cutters CrossFire owners have used successfully. Check the requirements above before you connect one.
 Vipercut 30 / 30i
30A max output
 Razorcut 45
45A max output
Sold by Langmuir
 Powermax 30/30XP
30A max output
 Powermax 45 SYNC
45A max output
Sold by Langmuir
 Powermax 65/65 SYNC
65A max output
Sold by Langmuir
 Powermax 85/85 SYNC
85A max output
Sold by Langmuir
 Powermax 105/105 SYNC
105A max output
 Powermax 125
125A max output
 Powermax 45/45XP
45A max output
 Powermax 380
27A max output
 Powermax 600
40A max output
 Powermax 800
50A max output
 Powermax 900
55A max output
 Powermax 1000
60A max output
 Powermax 1100
80A max output
 Powermax 1250
80A max output
 Powermax 1650
100A max output
 Max 42
40A max output
 Max 43
40A max output
 Cutmaster 38
30A max output
 Cutmaster 39
30A max output
 Cutmaster 42
40A max output
 Cutmaster 52
45A max output
 Cutmaster 60i
60A max output
 Cutmaster 81
60A max output
 Cutmaster 82
72A max output
 Cutmaster 102
100A max output
 Cutmaster 152
120A max output
 CutSkill 35A
35A max output
 CutSkill 70A
70A max output
 Spectrum 375 / 375 X-TREME
27A / 30A max output
 Spectrum 625 / 625 X-TREME
40A max output
 Spectrum 875
60A max output
 Spectrum 875 Auto-Line
60A max output
 Spectrum 2050
55A max output
 Tomahawk 375
25A max output
 Tomahawk 625
40A max output
 Tomahawk 1000
60A max output
 Tomahawk 1500
100A max output
 Procut 25
25A max output
 Procut 55
55A max output
 FORCECUT 40D
40A max output
 FORCECUT 42i
40A max output
 FORCECUT 62i
60A max output
 FORCECUT 82i
80A max output
 AirForce 27i
27A max output
 AirForce 40i
40A max output
 AirForce 400
27A max output
 AirForce 500i
27A max output
 AirForce 700i
40A max output
 PowerCut 900
60A max output
 PowerCut 1300
70A max output
 PowerCut 1600
90A max output
 PowerPlasma 50S
50A max output
 PowerPlasma 60S
60A max output
 PowerPlasma 80S
80A max output
 PowerPlasma 100S
100A max output
 Plasma 45
45A max output
 240V (v2.0, Black)
40A max output
 MicroCut 301
25A max output
 MicroCut 600
40A max output
 Microcut 875S
55A max output
 MA48
40A max output
 MA68
60A max output
 Plasma 375
40A max output
Choose by the thickest steel you cut regularly, using the cutter's clean-cut rating. The Razorcut 45 cuts cleanly to 1/2", the Powermax45 SYNC to 5/8", the Powermax65 SYNC to 3/4", and the Powermax85 SYNC to 1". Use the finder at the top of this page to get a recommendation for your table.
The CrossFire, CrossFire XL and CrossFire PRO work with the Razorweld Razorcut 45 and Hypertherm Powermax45 SYNC. The CrossFire PRO MAX and CrossFire XR work with every cutter we sell, up to the Powermax85 SYNC.
The Razorcut 45 is the budget choice and cuts steel cleanly to 1/2". The Hypertherm Powermax SYNC cutters cost more but have higher duty cycles, cleaner cuts at their rated thickness, and single-cartridge consumables. The Powermax45 SYNC also needs less air: 4 scfm at 90 psi, compared with 6.7 scfm at 75 psi for the Razorcut 45.
Your compressor must deliver the cutter's rated air flow continuously: 6.7 scfm at 75 psi for the Razorcut 45, 4 scfm at 90 psi for the Powermax45 SYNC, and 7.5 scfm at 85 psi for the Powermax65 and Powermax85 SYNC. Add a filter or dryer so moisture and oil don't shorten consumable life.
Yes. A straight machine torch mounts in the CrossFire torch holder. Every plasma cutter we sell includes a 25' machine torch, long enough for every CrossFire, including the XR. The Razorcut 45 is also sold with a hand torch, but that version is for manual cutting.
Usually, yes. It must use a blow-back start (never high-frequency start), we recommend a 220V cutter, and the torch lead must be at least 16' for the CrossFire PRO and 25' for the CrossFire XR. Check your model in the compatibility list on this page.
We don't recommend it. 110V plasma cutters require standoff distances that are too short for CNC cutting, so we only recommend 220V cutters for CrossFire tables.
Yes. Each CrossFire table's order section offers packages that include a plasma cutter and machine torch, ready to connect. You can also buy any cutter on this page on its own.